Técnicas de união
Joining Techniques
Texto da página
Link desta página: https://ranger.mbrace.com.br/carroceria/323
Imagem: https://ranger.mbrace.com.br/img/carroceria/323.webp
501-25-65
Body Repairs - General Information
501-25-65
DESCRIPTION AND OPERATION
No corrosion of the brazed seam.
Low erosion of the zinc coating in the joining
area.
Low level of heating and thus little warping.
Easy finishing of the brazed seam.
Good for bridging gaps.
Technicians performing MIG brazing must use a
Ford-certified MIG brazing device and must have
been given appropriatetraining on the brazing
techniques which are used.
Only use the Ford-approved brazing solder
SG-CuSi3 (SG-CuSi3Mn1).
Unless specified otherwise, a minimum gap of 30
mm must be maintained between the MIG brazed
seam and any adhesive bonds.
1
E135738
Des
Description
FULSW
ion
1
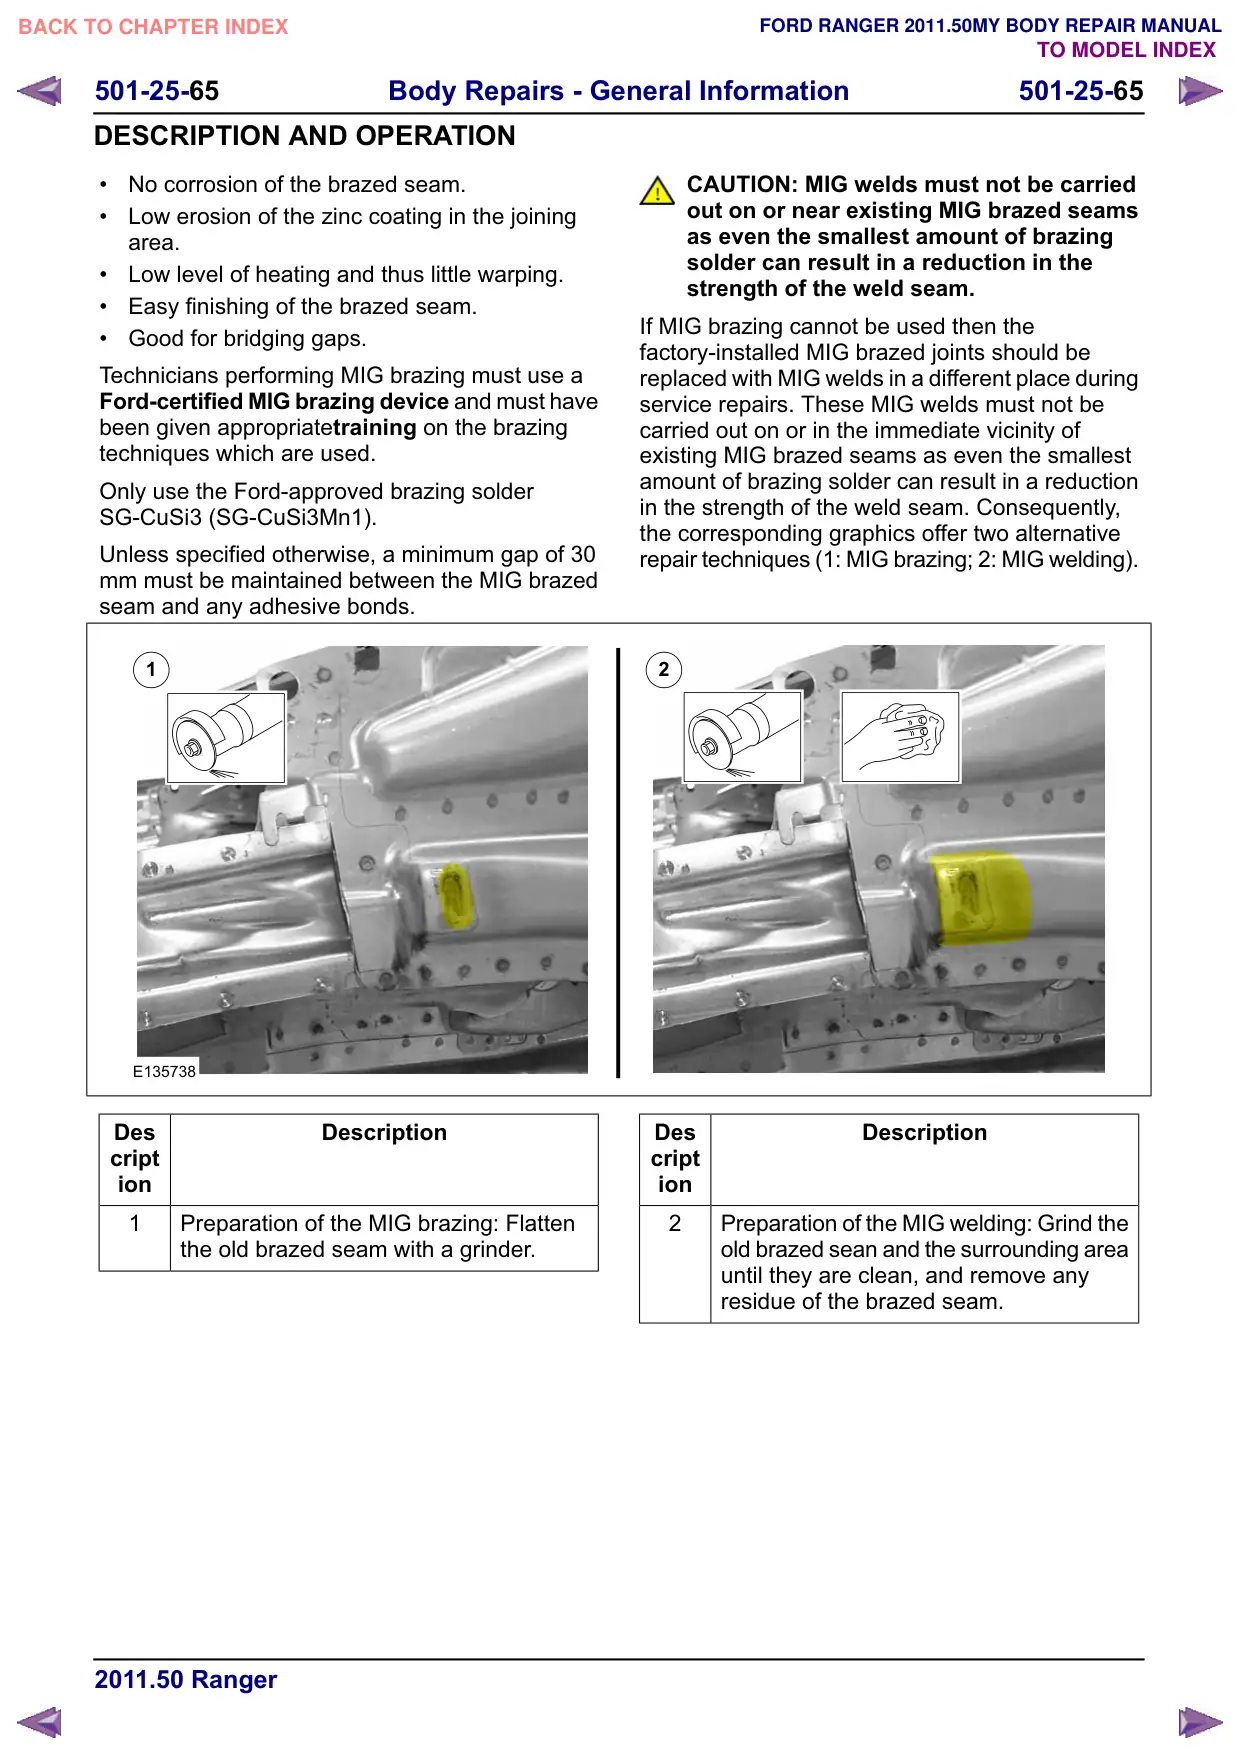
Preparation of the MIG brazing: Flatten
the old brazed seam with a grinder.
CAUTION: MIG welds must not be carried
out on or near existing MIG brazed seams
as even the smallest amount of brazing
solder can result in a reduction in the
strength of the weld seam.
If MIG brazing cannot be used then the
factory-installed MIG brazed joints should be
replaced with MIG welds in a different place during
service repairs. These MIG welds must not be
carried out on or in the immediate vicinity of
existing MIG brazed seams as even the smallest
amount of brazing solder can result in a reduction
in the strength of the weld seam. Consequently,
the corresponding graphics offer two alternative
repair techniques (1: MIG brazing; 2: MIG welding).
2
Des
Description
FULSW
ion
2
Preparation of the MIG welding: Grind the
old brazed sean and the surrounding area
until they are clean, and remove any
residue of the brazed seam.