Técnicas de união
Joining Techniques
Texto da página
Link desta página: https://ranger.mbrace.com.br/carroceria/319
Imagem: https://ranger.mbrace.com.br/img/carroceria/319.webp
501-25-61
Body Repairs - General Information
501-25-61
DESCRIPTION AND OPERATION
Special features to note when puddle welding:
The panels to be joined must lie perfectly flat to
one another.
The panel flanges must be treated with
corrosion protection. The position of the weld
must be bare.
Prepare the holes depending on the thickness
and number of the panels. The hole size should
be 6-10 mm, or match the original weld spot.
Start the welding procedure on the panel at the
bottom so that the hole is filled completely.
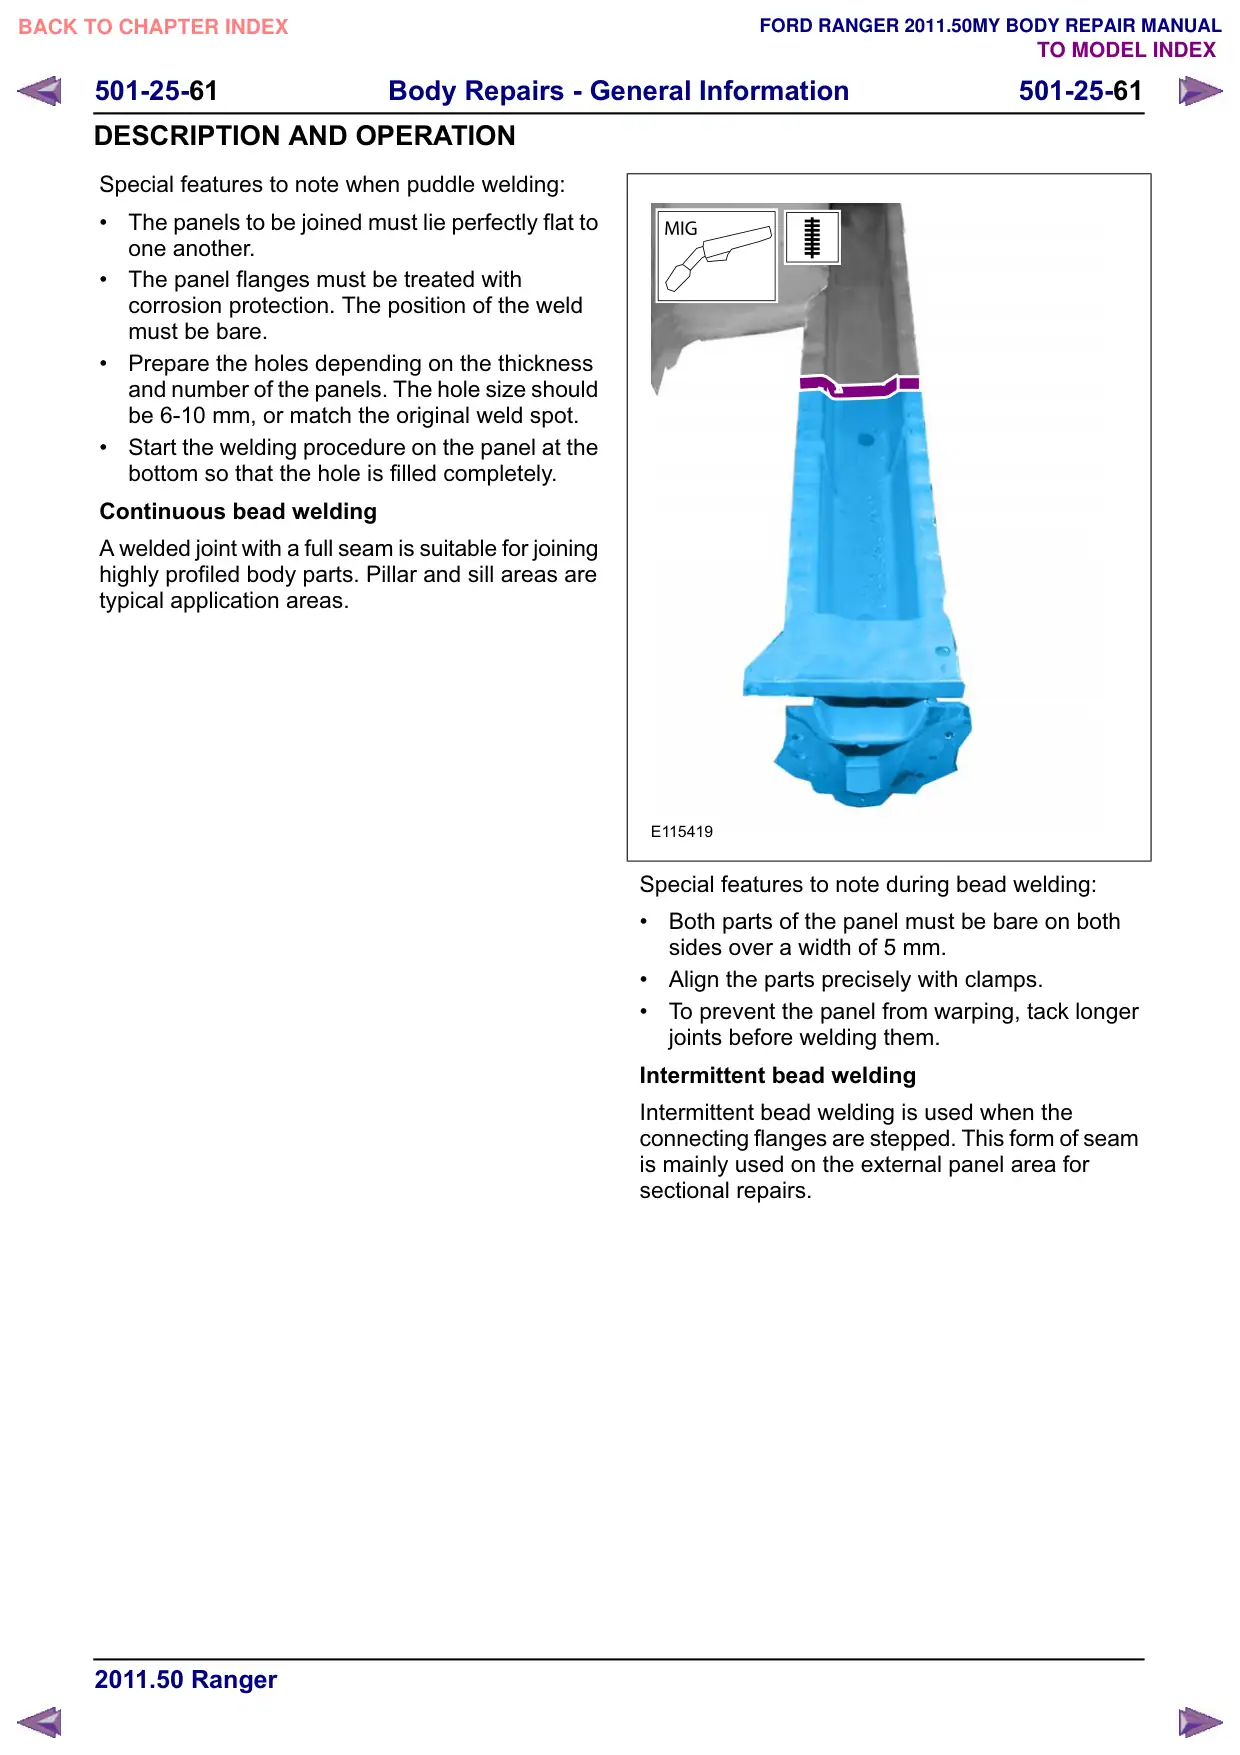
Continuous bead welding
A welded joint with a full seam is suitable for joining
highly profiled body parts. Pillar and sill areas are
typical application areas.
E115419
Special features to note during bead welding:
Both parts of the panel must be bare on both
sides over a width of 5 mm.
Align the parts precisely with clamps.
To prevent the panel from warping, tack longer
joints before welding them.
Intermittent bead welding
Intermittent bead welding is used when the
connecting flanges are stepped. This form of seam
is mainly used on the external panel area for
sectional repairs.