Coluna B e reforço – Cabine dupla
B-Pillar and Reinforcement – Double Cab
Texto da página
Link desta página: https://ranger.mbrace.com.br/carroceria/441
Imagem: https://ranger.mbrace.com.br/img/carroceria/441.webp
501-29-49
Side Panel Sheet Metal Repairs
501-29-49
REMOVAL AND INSTALLATION
Installation
1. NOTE: Before resistance spot welding of body
panels with a total panel thickness of 3 mm and
greater, the manufacturer's welding equipment
instructions and sub-section 501-25 must be
followed.
Refer to: Tools and Equipment for Body Repairs
(501-25 Body Repairs - General Information,
Description and Operation).
2. NOTE: Sealer or adhesive must not be applied
in welding zones. Areas which were bonded or
sealed needs to be thoroughly sealed
afterwards.
Refer to: Sealer, Underbody Protection Material
and Adhesives (501-25 Body Repairs -
General Information, Description and
Operation).
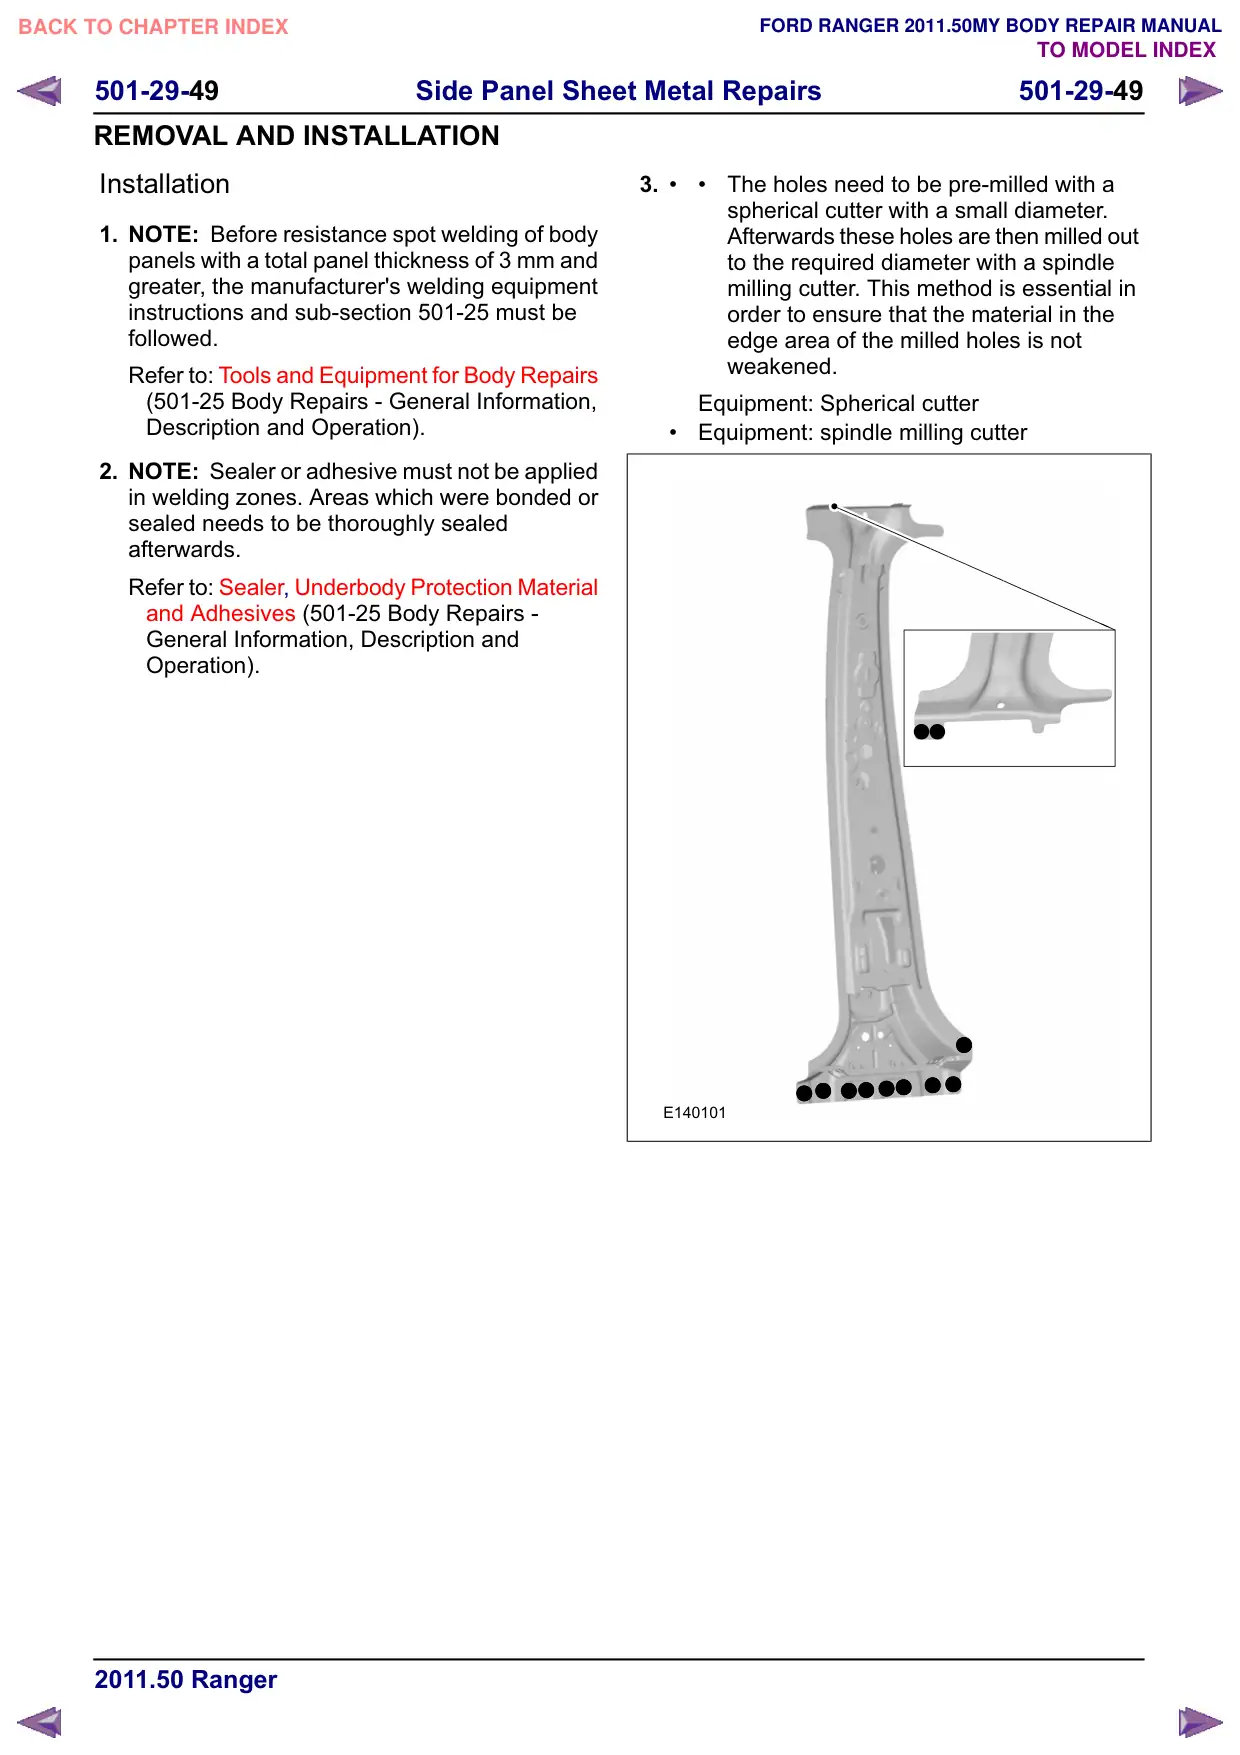
3.
The holes need to be pre-milled with a
spherical cutter with a small diameter.
Afterwards these holes are then milled out
to the required diameter with a spindle
milling cutter. This method is essential in
order to ensure that the material in the
edge area of the milled holes is not
weakened.
Equipment: Spherical cutter
Equipment: spindle milling cutter
E140101